Every architectural glass project faces a critical question during inspection: which defects warrant rejection, and which fall within acceptable tolerances? After two decades of producing extra-large structural glass—including record-breaking installations like the Zhangjiajie Grand Canyon Glass Bridge—we’ve learned that proper defect identification requires understanding both industry standards and real-world viewing conditions. This guide translates ASTM C1036 specifications into practical inspection criteria that protect quality without setting unrealistic expectations.
Understanding ASTM C1036 Inspection Standards
ASTM C1036-21 establishes the baseline for flat glass quality in North America. The standard defines acceptable visual characteristics through three critical parameters: viewing distance, angle, and lighting conditions. Inspections must occur at 10 feet (3 meters) distance, at angles between 45 to 90 degrees from the glass surface, under natural or office lighting of approximately 500 lux.
These conditions mirror how building occupants actually experience glass rather than laboratory scrutiny. When architectural glass spans 3.66 × 28 meters—our maximum production size for tempered glass—the 10-foot inspection distance ensures defects visible under normal use get flagged while microscopic imperfections that occupants would never notice get classified correctly as acceptable.

The standard distinguishes between “allowable” characteristics that don’t compromise performance and “defects” that affect structural integrity, thermal performance, or aesthetics beyond acceptable thresholds. This distinction matters because some visual characteristics result from manufacturing physics rather than quality failures.
Allowable vs Rejectable: Key Defect Categories
Inclusions and Foreign Material

Small inclusions under 1mm diameter that aren’t sharp or protruding typically meet ASTM acceptance criteria if they occur fewer than 5 per square foot when viewing from 10 feet. These microscopic bubbles or particles form during melting and pose no structural risk.
Rejectable inclusions include any foreign material larger than 3mm, sharp protrusions that could propagate cracks, or clustered defects exceeding the 5-per-square-foot threshold. In tempered glass installations—where we process up to 2,500 square meters daily—inclusions near edges raise additional concerns because they may interfere with tempering stress distribution.
| Defect Type | Acceptable Threshold | Rejection Criteria |
|---|---|---|
| Small inclusions | <1mm, ≤5 per sq ft | >3mm or sharp protrusions |
| Air bubbles | <3mm, not clustered | >5mm or visible at 10 ft |
| Edge contamination | <5mm from edge | Any penetration into viewing area |
| Clustered defects | Separated by >300mm | Multiple defects within 300mm |
Scratches and Surface Damage
Surface scratches present the most frequent gray area in glass inspection. ASTM C1036 permits light scratches not readily visible at the 10-foot inspection distance. In practice, scratches under 50mm length and not concentrated in the primary viewing area usually pass inspection.
Reject glass with scratches exceeding 75mm, deep gouges that catch a fingernail, or scratch patterns that create visible lines across the viewing field. For laminated glass—our 4.2 × 28-meter production line handles the industry’s largest sizes—scratches on interior surfaces between glass plies become permanently visible and warrant automatic rejection.
During our quality audits at the 140-acre Henan facility, we photograph borderline scratches under the specified lighting to eliminate subjective judgment. This documentation proves invaluable when disputes arise between fabricators, contractors, and architects.

Optical Distortion and Roller Wave
Roller wave—the periodic distortion created as glass passes over tempering rollers—challenges even experienced inspectors. ASTM allows slight roller wave provided it doesn’t cause objectionable distortion when viewing reflections or through-glass sightlines at 10 feet.
Quantifying “objectionable” requires the straightedge test: place a 300mm straightedge perpendicular to the roller wave pattern. If the gap between glass and straightedge exceeds 0.5mm, or if reflected images show pronounced waviness, reject the lite. For our 3.66 × 28-meter curved tempering line, roller wave becomes more critical in concave orientations where distortion amplifies.
Heat-strengthened glass typically exhibits less roller wave than fully tempered glass because of slower cooling rates. When specifications demand minimal distortion—museum vitrines, luxury retail storefronts—specifying heat-strengthened rather than tempered glass often provides better optical results while maintaining adequate strength.

Edge Quality Standards
Edge defects compromise both safety and aesthetics. ASTM C1036 addresses edge chips, ream (small fractures extending into the glass body), and shell (missing glass along the edge).
For tempered glass, chips larger than 6mm in any dimension require rejection because they indicate inadequate edge grinding before tempering. Ream extending more than 9mm from the edge similarly fails inspection. These thresholds balance manufacturing realities—minor edge imperfections occur during handling—against structural requirements, since edge defects concentrate stress and increase breakage risk.
Our 10 edge-grinding lines process up to 4,000 square meters daily through automated CNC systems that maintain consistent edge quality across extra-large lites. Even with automation, final inspection catches occasional defects that warrant rework or rejection before tempering. Once tempered, edge defects cannot be corrected without scrapping the entire lite.
| Edge Defect | Maximum Acceptable | Why It Matters |
|---|---|---|
| Chips | ≤6mm any dimension | Stress concentration points |
| Ream | ≤9mm from edge | Crack propagation risk |
| Shell | ≤13mm length, <25% thickness | Structural integrity |
| Grinding marks | Not visible at 10 ft | Aesthetic requirement |
Laminated Glass Appearance Standards
Laminated glass inspection follows ISO 12543-6 in addition to ASTM C1036. The standard addresses interlayer defects invisible in monolithic glass: bubbles, foreign particles, and delamination within PVB or SGP interlayers.
Acceptable interlayer bubbles measure under 10mm diameter with no more than 3 per square meter in the primary viewing area. Bubbles along the perimeter—within 25mm of edges—don’t count toward this limit because edge sealing naturally traps some air. For SGP-laminated structural glass, any delamination warrants rejection regardless of size because SentryGlas Plus provides the structural capacity, not just impact resistance.
Linear defects in interlayers—streaks or lines—cannot exceed 100mm length. During our laminated glass production on the 4.2 × 28-meter autoclave, humidity control and interlayer cleanliness determine defect rates more than any other factor. We maintain autoclave chamber humidity below 25% and clean interlayer surfaces with ionized air to minimize foreign particle introduction.

Low-E Coating Defects
Low-E coated glass presents unique inspection challenges because defects may affect thermal performance without obvious visual indicators. Cardinal CG Quality Guidelines—an industry reference beyond ASTM—specify allowable coating defects.
Pinholes in Low-E coatings under 1mm diameter don’t significantly affect insulating performance and remain acceptable if distribution doesn’t exceed 10 per square meter. Coating scratches follow similar criteria to glass scratches: not readily visible at 10 feet and not concentrated in primary viewing areas.
Reject glass with coating deletions (missing coating areas) exceeding 6mm, pronounced color variation across the lite, or any coating damage that exposes substrate glass. For our 3.3 × 28-meter coating line, real-time inspection systems flag coating defects during production, allowing operators to address process variations before significant material gets wasted.

Establishing Site-Specific Acceptance Criteria
While ASTM C1036 provides baseline standards, architectural projects often require tighter tolerances. Museum installations, high-end retail, and signature architectural features may specify “water white” low-iron glass with enhanced quality criteria.
Document project-specific requirements in shop drawings before fabrication begins. Specify maximum allowable defect counts per category, viewing distances that differ from 10 feet if applicable, and whether mock-ups require approval before full production. For the Shanghai Museum East Wing project, we produced sample lites demonstrating acceptable quality ranges before fabricating the full order—an investment that prevented disputes during final inspection.
Conversely, some applications permit relaxed criteria. Industrial glazing, warehouse installations, or glass in secondary viewing areas may accept defects that would fail inspection in primary locations. Clearly differentiating quality levels by application area controls costs without compromising performance where it matters.

Inspection Timing and Documentation
Inspect glass upon delivery, not after installation. ASTM C1036 explicitly states that glass acceptance occurs at the time of delivery and installation. Once installed, environmental factors—construction dust, weathering, adjacent work—can introduce defects unrelated to fabrication quality.
Photograph any questionable defects with a reference scale in the image. Note the defect location on lite identification labels. When rejecting glass, specify which ASTM criteria the defect violates rather than subjective judgments. This documentation protects all parties if disputes escalate to formal arbitration.
For extra-large structural glass installations, third-party inspection during fabrication—not just upon delivery—provides additional quality assurance. Many architects specify factory audits for projects using glass larger than 3 × 6 meters because shipping and installation risks increase exponentially with size.

FAQ
What’s the most commonly misunderstood glass defect criterion?
Roller wave causes more disputes than any other characteristic because “objectionable distortion” involves subjective interpretation. Using the straightedge test (0.5mm maximum gap) provides objective measurement, but architects and owners often have aesthetic expectations beyond ASTM minimums. Address expectations early with mock-ups showing acceptable roller wave for the specified glass type.
Can tempered glass scratches be polished out?
No. Once tempered, surface modifications break the surface compression that provides tempered glass strength. Any scratch visible after tempering must be accepted or the entire lite rejected and replaced. This is why pre-tempered quality control proves critical.
How do Low-E coating defects affect energy performance?
Small, isolated coating defects (pinholes, minor scratches) have negligible impact on insulating glass unit performance—less than 1% degradation. Large coating deletions or concentrated damage measurably reduce thermal performance and warrant rejection if the project has specified performance requirements.
Should inspection occur on site or at the fabrication facility?
Both. Fabrication facility inspections catch manufacturing defects before shipping. Site inspections upon delivery document any damage during transportation. Once installed, ASTM considers glass accepted unless installation damage caused obvious defects. Never wait until installation completion to inspect glass quality.
What documentation should accompany glass shipments?
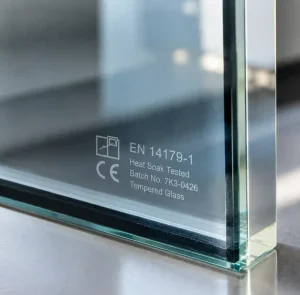
Each lite should include identification labels with fabrication date, glass type, coating orientation (if applicable), and quality control sign-off. For large projects, mill certificates documenting ASTM compliance and any third-party inspection reports provide additional quality assurance.
Conclusion
Glass defect identification balances technical standards with practical application requirements. ASTM C1036 provides the foundation, but successful projects require early alignment between fabricators, contractors, and design teams on acceptance criteria appropriate for each installation. The 10-foot, 45-degree, 500-lux inspection protocol eliminates most ambiguity, yet gray areas remain where professional judgment and documentation prove essential.
At Zhongbo Glass, our quality systems evolved through fabricating some of the world’s largest structural glass installations—projects where defect identification couldn’t rely on replacing small lites easily. We learned that photographing borderline defects, maintaining detailed inspection records, and proactively communicating with project teams prevents disputes more effectively than perfect fabrication alone. For architects and contractors specifying architectural glass, understanding which defects genuinely compromise performance versus which reflect manufacturing realities keeps projects on schedule while maintaining appropriate quality standards. Read more about our quality control procedures and edge finishing standards.